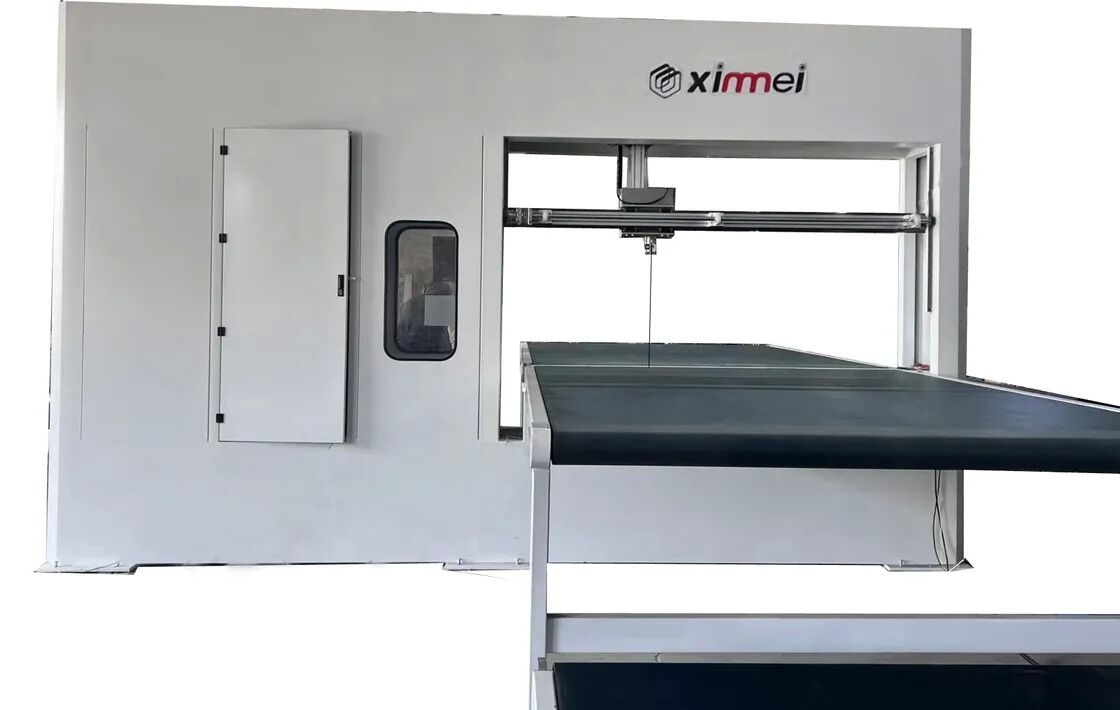
3000x2200 mm CNC Foam Contour Cutting Machine with 1300 mm Cutting Height and ±360° Band Blade Turning Angle
The TDPH-2.3 is an automatic CNC contour cutting machine built around a continuously circulating band knife instead of an oscillating blade. The band runs in one direction at up to 70 m/min and the cutting head rotates through ±360°, so the blade follows an irregular profile without lifting, turning or repositioning the block.
The working envelope covers blocks up to 3000×2200 mm with a cutting height of 1300 mm, which matches the output of standard batch foaming and block-cutting lines. Positioning tolerance is held at ±0.5 mm. Total motor power is 8.5 kW and machine weight is 3000 kg, carried on a frame of 6500×5000×3200 mm that is built to absorb the load of a full block and the pull of a fast-moving band.
The machine handles the soft foam families that make up the bulk of contour work: PU sponge, EPE pearl cotton, PE and EVA, plus laminated blocks of these materials once the adhesive lines are fully cured. Because the blade cuts instead of melting, the cell walls at the cut face stay open and bondable for the next lamination or gluing step.
Typical buyers are packaging plants, furniture and mattress factories, luggage and footwear material suppliers, and foam converters that need repeatable contour output at volume. An optional pressure roller holds tall, soft or laminated blocks against the table when the head changes direction.
What the Machine Does in the Line
A production cycle is a program recall rather than a manual setting, which is the main difference from a hand-shaped contour process.
- Load the block. A squared block is placed on the 3000×2200 mm table against the reference position.
- Lower the roller if fitted. The pressure roller holds the workpiece down for the whole pass.
- Recall the part program. The stored contour for that part number is selected from the control interface.
- Set blade speed and feed. Values are chosen for the foam grade — higher on long straight sections, lower through tight radii.
- Run the contour. The head rotates through ±360° so the blade edge always faces the direction of travel, and the profile is completed in one pass.
- Unload and repeat. The head returns to the load position, the part is removed, and the next block runs on the same program.
Programs are stored by part number, so a shape repeats across shifts without re-teaching. That is what separates a CNC contour machine from a manual template: the part is data, not a skill held by one operator.
How a Circulating Band Knife Cuts
A circulating band knife is an endless steel band running over two large wheels. The cutting section of the band passes through the workpiece while the return section runs behind the machine guard. Because the band moves continuously in one direction, the cut is smooth and uninterrupted: no reciprocating stroke, no dead point at the end of each oscillation and no reversal shock at the blade guides.
That continuous motion is the reason for the speed difference. An oscillating blade spends part of every stroke reversing direction, so only a fraction of the cycle is spent cutting. A circulating band uses the full cycle. On the same profile, our comparison shows a cycle roughly seven to eight times shorter than an oscillating knife machine, and the gain grows on shapes with long curves.
The ±360° rotation is the second capability. The cutting head turns the band around the vertical axis, so the edge always leads the direction of travel. The operator does not rotate the block and the profile does not need several passes: the machine follows the programmed path and the control system keeps the blade orientation correct.
The result is an edge that behaves like cut foam, not like processed foam. There is no melted skin, no burnt odour and no hardened rim, so adhesive penetrates the face instead of sitting on a glazed surface. There is also no wire to consume and no fume extraction to run, which keeps the running cost and the workplace simple.
Machine Structure and Key Components
- Circulating band knife unit: an endless steel band driven at 0–70 m/min, with tensioning and tracking systems that keep the band centred on the wheels during long runs.
- ±360° rotating cutting head: servo-controlled rotation that keeps the blade edge aligned with the direction of travel, so a complex contour is finished in one pass.
- CNC motion system: interpolated X/Y movement with acceleration profiles tuned for foam, so the head does not tear the material when it enters a corner or changes radius.
- Working table: a 3000×2200 mm support surface sized for full blocks, with the clearance needed under the 1300 mm cutting height.
- Optional pressure roller: a driven or non-driven hold-down that keeps tall and soft blocks in contact with the table and prevents lifting when the head changes direction.
- Control cabinet and operator interface: stores part programs and cutting parameters, with production counters and fault diagnostics.
- Safety guarding and interlocks: the band return path and the drive wheels are enclosed, and the cycle cannot start if a guard is open.
The structure matters as much as the control system. A band moving at 70 m/min pulls on the frame continuously, and any flex in the structure would appear as a wander in the profile. The 3000 kg base and the rigid frame are there to keep the blade path stable when the head is working at the far end of a 3000 mm block.
CNC Control, Blade Rotation and Edge Quality
One Pass for the Full Contour
The head rotates through ±360°, so the blade leads the travel direction and the block stays where it was loaded.
±0.5 mm Repeatability
Servo feed, close blade guidance and a stored program hold the profile from the first part to the last of the batch.
Open, Bondable Cut Face
The band separates the foam cells without melting, so adhesive penetrates the face and the laminate holds.
Accuracy comes from three things working as one system: the band is guided close to the cutting point, which limits sideways deflection; the servo feed advances at a constant rate through curves instead of following the speed of a hand; and the pressure roller, when fitted, keeps the block from creeping away from the datum.
The program reference is the table plane. Every shape is cut relative to that datum, which is why a squared block matters. If the base of the block is sloped, the contour is still correct in plan, but the wall height varies around the part and the error appears downstream at assembly.
Technical Specifications
| Parameter |
Specification |
| Model |
TDPH-2.3 |
| Cutting size |
3000×2200 mm |
| Cutting height |
1300 mm |
| Band blade running speed |
0–70 m/min |
| Precision tolerance |
±0.5 mm |
| Band blade turning angle |
±360° |
| Total motor power |
10 kW |
| Machine weight |
3000 kg |
| Overall dimension (L×W×H) |
6500×5000×3200 mm |
| Pressure roller |
Optional |
| Certification |
CE |
The 3000×2200 mm figure is the plan size of the block that can be processed; the 1300 mm figure is the wall height that can be cut in a single pass. Parts taller than that are cut in two operations or from a pre-split block.
Materials and Material Limits
The machine works with the flexible and semi-rigid foams used in packaging, furniture and footwear production:
- PU flexible foam: cushions, mattress layers, packaging inserts and convoluted profiles.
- EPE pearl cotton: protective packaging, fragile-goods inserts and laminated sheets.
- PE foam: construction, sports and protective packaging components.
- EVA: shoe soles, sports mats, tool inlays and costume parts.
- Laminated foam blocks: where the adhesive is fully cured and the layers are compatible with band cutting.
Two limits should be stated clearly before an order. The machine is not intended for foam containing hard inclusions, abrasive fillers, metal inserts or uncured adhesive layers; those materials damage the band and the guide inserts. And on very small radii in extremely soft, low-density foam, a band under tension can compress the material, which is the one case where an oscillating knife may give better control.
Density affects feed rate more than any other property. Low-density EPE runs at a high feed through long curves, while a dense PU part with tight corners is run slower so the band can follow the path without pushing the foam ahead of the blade.
Typical Applications
- Packaging: custom-shaped EPE and PU inserts, shock buffers, trays and cradles for electronics, instruments and glassware, where one profile repeats thousands of times and cycle time decides the cost per part.
- Furniture and cushions: irregular PU cushions, sofa and chair arm profiles, mattress transition layers and shaped accessories, including rounded contours that would need several setups on a fixed-blade machine.
- Luggage and footwear: EVA and PE shaped blanks for luggage lining, shoe padding, insoles and sports protection, where tight radii meet soft material.
- Foam converting: volume profiling of large special-shaped blocks, replacing hand cutting or several passes on slower equipment.
- Upgrade path: plants that already run a vertical block cutter and a peeling line but still shape profiles by hand.
In all of these cases the commercial argument is the same: the shape is a program, so a design change costs setup time instead of a new die.
Comparison with Oscillating Knife, Hot Wire and Die Cutting
| Method |
Strength |
Limit |
| Circulating band knife (TDPH-2.3) |
Continuous one-direction cut, ±360° head rotation and 0–70 m/min; one pass for complex contours |
Needs a squared block; very small radii in very soft foam need reduced feed |
| Oscillating knife |
Good control on very small radii and some very soft grades |
Stroke reversal limits speed on long contours; multiple setups on complex shapes |
| Hot wire |
Low purchase cost for straight cuts and simple shapes |
Melted, hardened edge; wire consumption and fumes; poor adhesive bond |
| Die cutting |
Fast for very high volume of one small part |
Die cost and storage; a design change waits for a new die |
The choice usually comes down to volume and shape complexity. For a packaging program that repeats one contoured insert in large numbers, the circulating band wins on cycle time and tooling cost. For a workshop cutting a handful of very small radii in ultra-soft foam, an oscillating knife may still be the better instrument. Many plants keep both and route work by part size.
Pressure Roller Option and Holding Methods
Tall foam blocks are light for their size, and a fast-moving band can lift or shift them when the head changes direction. The optional pressure roller holds the workpiece against the table across the width of the cut.
It is recommended in three situations: blocks above roughly 800 mm in height, very soft or low-density grades, and laminated blocks where a layer could separate if the block moved. For thin, dense or short parts the roller is often unnecessary, and the machine runs without it.
For parts that cannot be held by a roller, a simple fixture or a sacrificial base board can be used. The program reference is the table plane, so any fixture height has to be accounted for in the setup. Sharing the part drawing and the foam grade before the order lets us confirm if the roller is needed and which holding method suits the part.
Position in the Foam Production Line
The TDPH-2.3 sits in the shaping stage. Upstream it receives squared blocks from a foaming line, a horizontal peeling machine or a vertical block cutter. Downstream its output feeds lamination, gluing, quilting, upholstery or packaging assembly.
The link to the previous process matters more than buyers expect. The block should have a flat bottom and reasonably square sides, because the table and the roller need a stable reference and the program assumes a known datum. A sloped block produces a part with a varying wall height even if the contour in plan is correct.
In a typical layout a vertical cutter squares the block, the TDPH-2.3 cuts the contour, and a lamination line bonds the shaped part to fabric or to another foam layer. Where the plant also runs a peeling machine, thin sheets can be peeled first and profiled afterwards, which is often more economical than cutting thin sections from a full block.
Site Requirements: Power, Floor and Space
- Foundation: a level, reinforced concrete floor able to carry the 3000 kg machine plus the workpiece; anchor points are supplied.
- Power: a dedicated supply matching the 8.5 kW connected load, with correct earthing and stable voltage.
- Space: access to the 6500×5000×3200 mm footprint from the loading side, with room for safe blade changes and for the control cabinet door to open fully.
- Environment: a dry, covered area. Foam dust should be cleared regularly, because dust on the guides and the band wheels is the usual cause of tracking faults.
Because of the frame size, the shipping route should be checked at order stage: the machine may need a flat-rack container depending on the destination and the inland transport.
Operation, Safety and Training
The band wheels and the return section of the blade are enclosed by guards with interlocks, and the control system prevents the cycle from starting if a guard is open. Emergency halt buttons are placed at the operator position and at the rear of the machine.
Blade changes are carried out with the drive isolated and with cut-resistant gloves. Because the band is a continuous loop, correct tensioning and tracking after a change are essential, and the procedure is covered in the operation manual.
Operation is learned quickly. A new operator normally needs one to two days to load programs, set the roller and blade speed, and run a first article. Programming is done offline from a DXF file or a drawing and transferred to the controller, so no machine-side code writing is required. Training at installation, a printed manual and remote support for program preparation are included.
Maintenance, Band Life and Spare Parts
- Daily: band tension, band condition, guide cleanliness and roller pressure.
- Weekly: wheel tracking, guide wear, lubrication points and electrical connections.
- Consumables: band knives, guide inserts, wheel bearings, tension springs and proximity sensors.
Band life depends on foam density and filler content, and a well-run machine normally gives weeks of production per band. When the cut edge starts to show fuzz or the feed force rises, the band is re-sharpened or replaced. Bands can be re-sharpened several times before they are retired.
Wheel tracking and guide wear are the second maintenance items to watch, because they open the tolerance gradually rather than failing at once. A weekly tracking check catches the drift before it shows in the finished parts.
Quality Control, Packaging and Delivery
Each machine is assembled, wired and run before shipment. The test record covers band tracking and tension, head rotation through the full 360 degrees, servo response, guarding, emergency halt function and a sample contour cut measured against the drawing. The inspection record is supplied with the machine.
The machine ships in export-grade packaging: the table and frame are protected against moisture, the cutting head is secured, and loose parts are boxed and labelled. Packaging details are confirmed before dispatch because the 6500×5000×3200 mm frame may need a flat-rack container depending on the route.
Delivery is 45 working days after the down payment is confirmed, shipped from Qingdao port. Payment terms are L/C or T/T, minimum order quantity is one set, and supply ability is three sets per season. The electrical configuration is CE compliant for European and other export markets.
Frequently Asked Questions
Q: How much faster is a circulating band than an oscillating knife machine?
A: On the same profile, our comparison shows a cycle roughly seven to eight times shorter, because the band runs continuously in one direction and there is no reversal dead time. The gain is higher on long curves and lower on very small radii.
Q: Can it cut a full 360-degree contour without rotating the block?
A: Yes. The cutting head rotates the band through ±360° and keeps the edge aligned with the travel direction, so the block stays in place and the profile finishes in one program.
Q: What if my block is larger than 3000×2200×1300 mm?
A: It cannot be loaded as one piece. The block should be squared on a vertical or horizontal cutter first, or split into sections. If the bulk of your production exceeds this envelope, tell us the actual size and we will advise on a larger configuration.
Q: Do I need the pressure roller?
A: It is recommended for blocks above roughly 800 mm in height, for very soft or low-density foam and for laminated blocks. For thin, dense or short parts it is often unnecessary. Share the part profile and material and we will advise.
Q: How often does the band knife need changing?
A: Band life depends on density and filler content, and users normally run for weeks between changes. Bands can be re-sharpened several times. Keep one spare band on site so a damaged edge does not hold up the line.
Q: Can the finished parts go straight into lamination or packing?
A: Yes. The band cut leaves an open cell face that bonds well with adhesive, and ±0.5 mm is normally tight enough for direct assembly. For automated lines we can discuss output handling and part stacking with your process team.
Q: What is needed on site before installation?
A: A level reinforced floor able to carry 3000 kg plus the workpiece, a dedicated 8.5 kW supply with correct earthing, and access around the 6500×5000×3200 mm footprint for loading and blade changes.
Request a Quotation for the TDPH-2.3
Tell us the block size you start from, the smallest radius and minimum part size, the foam grades and densities, the output you need per shift and the downstream process. We will confirm the configuration, if a pressure roller is needed, the power requirement and the delivery schedule, and we can arrange sample cuts on your material before the order.


 Your message must be between 20-3,000 characters!
 english
 français
 Deutsch
 Italiano
 Русский
 Español
 português
 Nederlandse
 ελληνικά
 日本語
 한국
 العربية
 हिन्दी
 Türkçe
 indonesia
 tiếng Việt
 ไทย
 বাংলা
 فارسی
 polski