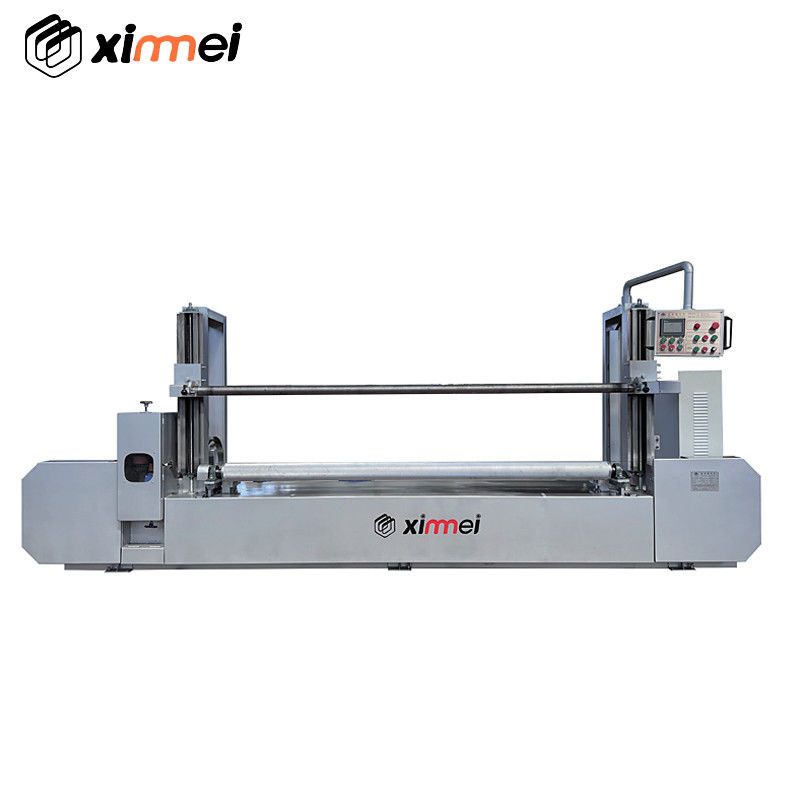
Cylindrical Foam Peeler Sponge Roll Peeling Machine for 20-1500 mm Rolls
TDPA-2300 Cylindrical Foam Peeler for Sponge Roll Peeling
The TDPA-2300 is a rotary peeler built around one job: taking a cylindrical foam roll and turning the outside of it into a continuous thin sheet. Rolls from 20 mm to 1500 mm in diameter and up to 3000 mm wide can be chucked and peeled, with sheet thickness from 1 mm to 30 mm set on the CNC touch screen and held to ±0.08 mm on 1-3 mm sheet. Peeling speed is 0-130 m/min, the drive is 8.69 kW, machine weight is 2000 kg and the footprint is 5000*2500*2000 mm.
Cylinder peeling is a tolerance problem before it is a speed problem. The roll has to turn true on its own axis, the blade has to hold depth against a surface that is not perfectly round, and the sheet has to leave without tearing as the diameter shrinks. The TDPA-2300 answers each of those with a servo-controlled head, a guide that holds the depth reference and a peeling action that shears rather than compresses the foam.
TDPA-2300 peeling a PU cylindrical foam roll into a continuous thin sheet.
The Machine at a Glance
20-1500 mm roll range
One chuck arrangement covers small PU cylinders and 1500 mm mattress blocks without a second machine.
±0.08 mm on 1-3 mm sheet
The guide holds the depth reference while the blade shears, so the sheet does not thin out as the roll runs down.
1-30 mm by touch screen
Sheet thickness is typed, not geared, so a change of size costs one setting and one test sheet.
Model: TDPA-2300
Control: CNC touch screen
Cutting thickness: 1-30 mm
Cutting tolerance: ±0.08 mm (1-3 mm sheet)
Cutting speed: 0-130 m/min
Cutting diameter: 20-1500 mm
Cutting width: 500-3000 mm
Motor power: 8.69 kW
Machine weight: 2000 kg
Overall dimension: 5000*2500*2000 mm
Certification: CE
Cylindrical roll chucked on the cutting bed before the peeling pass.Machine overview: touch screen, peeling head and take-off side.
Peeling a Cylindrical Roll Step by Step
Check the roll. Measure the diameter and trim any torn or sloped end face before chucking.
Chuck and true up. Mount the roll, then turn it by hand and watch for run-out at the far end.
Enter the thickness. Set 1 mm to 30 mm on the touch screen for the sheet you need.
Set the speed. Pick a peeling speed within 0-130 m/min that suits the foam density.
Peel the outside. Start the head and take the sheet off continuously as the roll diameter reduces.
Re-chuck for the next roll. The thickness setting stays, only the roll changes.
The first metre of every roll is the sample. If it measures within the tolerance band at both edges and in the middle, the rest of the roll will follow, provided the guide has not moved and the blade is still sharp.
Holding Tolerance as the Diameter Shrinks
A cylindrical roll does not present a perfect surface to the blade. Moulded foam has a skin, the roll may be slightly oval, and the diameter reduces with every metre peeled. If the depth reference came from the roll surface, the sheet would follow every irregularity. On the TDPA-2300 the head is referenced to the guide, so the cut follows the machine geometry instead of the foam.
Run-out is the other half of the problem. A roll that is not turning true produces a sheet that is thick on one side and thin on the other, and no thickness setting can correct it. Check the far end of the roll by hand before the pass; a 0.5 mm wobble on a 1500 mm roll shows up as a visible thickness difference across a 3000 mm wide sheet.
The last part of the roll is where thin sheet gets difficult. As the diameter drops, the surface speed at the blade falls, and the sheet can lift. Reducing the feed rate near the end of the roll, or re-chucking the remaining core, keeps the last metres inside tolerance instead of selling them as scrap.
Square the roll: a sloped end face is the most common cause of a wavy first metre.
Watch the core: below 100 mm diameter, slow the feed and support the sheet at take-off.
Gauge the first metre: measure both edges and the middle, not just the centre.
On 1-3 mm sheet the tolerance is ±0.08 mm. On thicker sheet the practical band widens with foam density, which is why the sample is measured before the batch, not after.
Cutting head and guide: depth is referenced to the machine, not the roll surface.
Technical Parameters
Parameter
Value
Model
TDPA-2300
Cutting width
500-3000 mm
Cutting diameter
20-1500 mm
Cutting thickness
1-30 mm
Cutting tolerance
±0.08 mm (1-3 mm sheet)
Cutting speed
0-130 m/min
Motor power
8.69 kW
Machine weight
2000 kg
Overall dimension (L*W*H)
5000*2500*2000 mm
Certification
CE
Core Advantages
Built for cylinder work: the chuck and the peeling head are aligned for rolls from 20 mm to 1500 mm diameter, from PU cylinders to full mattress blocks.
Tolerance that survives the roll: depth is referenced to the guide rather than to the roll surface, so the sheet thickness holds as the diameter reduces.
Clean cut face: rotary shearing leaves a flat face without the blade marks a reciprocating cut can leave on soft foam.
No gear change: 1 mm to 30 mm is entered on the touch screen, which removes the trial cut and the scrap that follows a mechanical changeover.
Thin sheet capability: peeling down to 1 mm opens the comfort layer and packaging grades that a thicker slicer cannot reach.
Simple handling: a finished roll is re-chucked in minutes, which matters when a batch is made of short cylinders.
Low maintenance load: the rotary head has few wearing parts, and the parts that do wear are the blade and the guide.
Primary Applications
PU cylinder conversion: peeling moulded foam cylinders into sheet for cushions and pads.
Mattress and furniture: comfort layers and padding peeled from round foam buns.
Packaging: thin protective foam peeled from foam roll stock.
Sound and thermal insulation: uniform foam sheet for lining and insulation builds.
Automotive trim: thin foam for interior padding and trim backing.
Foam conversion trade: sheet peeled to a resale thickness from bought-in rolls.
Sheet emerging from the blade as the roll diameter reduces.
Cylinder peeling in production on a TDPA-2300.Peeled sheet stacked flat for cushion, padding and packaging use.
Common Peeling Faults and Fixes
Symptom
Likely cause
Action
Sheet thicker at one end
Roll not centred on the chuck
Re-chuck and check the roll run-out before the pass
Thickness drifts during a roll
Knife dulling or guide play
Check the edge, reset the guide clearance
Torn or chattered cut face
Feed speed too high for the foam grade
Lower the speed setting for soft or low-density foam
Visible marks on the sheet
Blade vibration or loose band tension
Retension the blade, check the drive pulley
Sheets stick and tear on take-off
Static and foam dust on the table
Clean the table, check dust extraction
Machine alarms at start
Thickness set outside the 1-30 mm window
Re-enter the value inside the working range
Most thickness complaints come from the first metre of a roll. Check that metre before running the rest of the batch, and one rejected sheet replaces half a shift of scrap.
Operation, Safety and Workshop Conditions
The machine runs on a 8.69 kW drive and weighs 2000 kg, so it needs a level floor and clear space at the take-off side. A 3000 mm wide sheet needs a table and a stacking route as wide as the machine, otherwise the operator stops the pass to fold the sheet and the tolerance is lost at the crease.
Foam stiffness changes with temperature. A cold roll peels harder and a warm one compresses more easily, so check the first sheet after a temperature change in the hall and note it in the batch log. For soft grades, the same thickness setting can behave differently in the morning than after the heating comes on.
Guarding: keep the peeling head guard in place and the emergency stop within reach of the take-off position.
Chucking: never adjust a roll on the machine axis while the head is running.
Dust: run the extraction whenever the foam generates dust; loose foam dust packs into the guide and opens the tolerance.
Handling: use a lift or a roll cradle for 1500 mm rolls instead of tipping them onto the chuck.
Roll peeling in progress with the sheet taken off continuously.
Blade Care and Daily Maintenance
The blade and the guide are the two parts that decide output quality. Check the blade edge every shift, keep the guide free of dust and re-set the guide with a gauge after every blade change. Setting the guide by feel is the most common cause of a tolerance complaint in the first week after a service.
Chuck jaws and the roll axis take the handling load, so check them for wear when a roll starts to show run-out even though the end face is square. Grease points and the electrical cabinet are routine work and should be on the weekly list rather than left to a breakdown.
Every shift: blade edge, guide clearance, dust on the head and the take-off table.
Monthly: lubrication, cabinet dust, thickness check against a gauge on a test roll.
After a blade change: re-set the guide, then peel one test roll before the batch.
Cutter and guide detail: re-set with a gauge after every blade change.
Packaging and Delivery
The machine ships in an export plywood case with the peeling head blocked, the chuck protected and blades packed separately. At 5000*2500*2000 mm and 2000 kg, check the container loading plan and the door width at the destination before the booking is confirmed.
Lead time is 45 working days after downpayment, payment terms are L/C or T/T, and the minimum order quantity is one set. Remote commissioning support, installation guidance and spare blades can be shipped with the machine.
CE electrics, guarding and emergency stop checked before packing.
Frequently Asked Questions
Q1: What roll diameters can the machine peel?
A: 20 mm to 1500 mm in diameter, with a cutting width of 500-3000 mm.
Q2: What is the thinnest sheet it can produce?
A: 1 mm, with ±0.08 mm tolerance held on the 1-3 mm range.
Q3: Does the sheet thickness change as the roll gets smaller?
A: No, provided the roll turns true. The head is referenced to the guide, not to the roll surface.
Q4: How is the thickness adjusted?
A: On the CNC touch screen, 1 mm to 30 mm, with no gear change and no mechanical gauge.
Q5: What about very soft foam?
A: Reduce the peeling speed within the 0-130 m/min range; a slower pass gives a flatter face on low-density foam.
Send Your Peeling Requirement
Tell us the foam type, roll or block size, target sheet thickness and expected output per shift. We will confirm the TDPA-2300 configuration, quote the machine and share the delivery schedule. Spare blades, guides and remote commissioning support are available with every order.


 Your message must be between 20-3,000 characters!
 english
 français
 Deutsch
 Italiano
 Русский
 Español
 português
 Nederlandse
 ελληνικά
 日本語
 한국
 العربية
 हिन्दी
 Türkçe
 indonesia
 tiếng Việt
 ไทย
 বাংলা
 فارسی
 polski