Product Details
Place of Origin: Qingdao
Brand Name: Xinmeiteng
Certification: CE
Model Number: C518
Payment & Shipping Terms
Minimum Order Quantity: 1 Set
Price: Inquiry
Packaging Details: TO BE DETERMINED
Delivery Time: 45 working days after downpayment
Payment Terms: L/C,T/T
Supply Ability: 3 sets per season
Motor Power: |
3.7 KW |
Hole Diameter: |
50-80 Mm |
Bore Hole Length: |
500-2300 Mm |
Sponge Diameter: |
1200-1500 Mm |
Machine Weight: |
2000 Kg |
Overall Dimension: |
6500*2000*2500 Mm |
Motor Power: |
3.7 KW |
Hole Diameter: |
50-80 Mm |
Bore Hole Length: |
500-2300 Mm |
Sponge Diameter: |
1200-1500 Mm |
Machine Weight: |
2000 Kg |
Overall Dimension: |
6500*2000*2500 Mm |
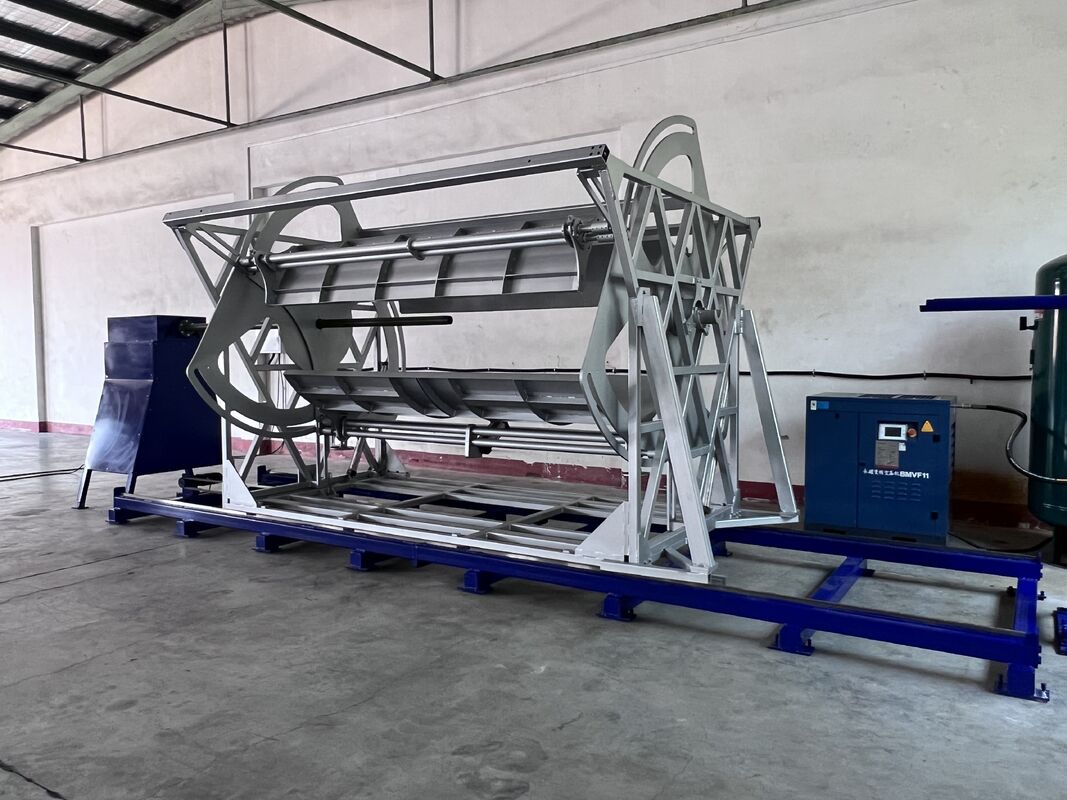
The C518 is a foam drilling machine with 3-direction clamping and automatic center positioning. Bore hole length is 500-2300 mm, hole diameter is 50-80 mm, sponge diameter is 1200-1500 mm, motor power is 3.7 kW, machine weight is 2000 kg and the overall dimension is 6500*2000*2500 mm.
A round roll is the hardest workpiece to hold. Clamping from one direction pushes the roll out of line, and the bore follows the roll. Three-direction clamping holds the roll from above and both sides, so the centre stays where it was set before the cutter enters.

Holds the roll from above and both sides.
The machine locates the centre line before boring.
Covers the cylindrical blocks used on peeling lines.
Full-length bores in a single pass.


Check the bore at the exit as well as the entry. A roll that was not clamped square shows a difference between the two ends.
A cylindrical roll has no flat face to register against. A single clamp pushes it away, and a two-direction clamp still lets it rotate. Three-direction clamping holds the roll on both sides and from above, which fixes the position before the cutter starts.
Automatic centring builds on that. Once the roll is held, the machine locates the centre line, so the operator does not judge the centre by eye. That removes the variation between one roll and the next, which is what matters on a batch.
The result is a bore that is in the same place on every roll. Shafts fit consistently, and the peeling line receives rolls that sit straight rather than rolls that rock on the shaft.

| Parameter | Value |
|---|---|
| Model | C518 |
| Machine type | 3-direction clamping foam drilling machine |
| Bore hole length | 500-2300 mm |
| Hole diameter | 50-80 mm |
| Sponge diameter | 1200-1500 mm |
| Clamping | 3-direction clamping |
| Positioning | Automatic center positioning |
| Motor power | 3.7 kW |
| Machine weight | 2000 kg |
| Overall dimension | 6500*2000*2500 mm |
| Certification | CE |


| Symptom | Likely cause | Action |
|---|---|---|
| Bore runs off centre | Roll not clamped square or centre height wrong | Re-clamp the roll and reset the centre height |
| Hole diameter out of tolerance | Worn or damaged cutter head | Fit a new cutter head and re-check |
| Thread damaged at the entry | Threading feed too fast | Reduce the threading feed rate |
| Roll slips during boring | Clamp pressure too low | Increase clamp pressure and check the pads |
| Spindle vibration | Worn bearing or loose drive belt | Check bearing play and belt tension |
| Torn bore surface | Dull cutter or feed too fast | Replace the cutter and reduce the feed |
Boring faults on a clamped drilling machine are usually set-up faults. Check clamping, centre height and cutter condition before adjusting the machine, because those three cause most rejects.
Keep hands clear of the clamps when they close. Three-direction clamping closes from several sides at once, and the gap between the roll and the pad is small.
Stop the spindle before releasing the clamps. A roll that is released while the cutter is turning can move against the cutter.

The clamp pads and the centring system are what hold accuracy. Check the pads for wear monthly and verify the centring position against a known roll after any adjustment.
The cutter head and spindle need the usual checks. A dull head tears the bore wall and loads the spindle, which shows up as vibration before it shows up as a dimension error.

The machine ships in a reinforced export crate with the frame and clamping units braced for transport, sized to the 6500*2000*2500 mm envelope.
The shipment includes the clamping specification, layout drawing and a commissioning checklist, with remote support during installation.

A: The roll is held from above and from both sides during boring.
A: 1200-1500 mm sponge diameter.
A: Automatically, by the machine's centring system.
A: 500-2300 mm in a single pass.
Tell us the foam type, block or roll diameter, required hole diameter and the boring length you need. We will confirm the machine configuration, quote it and share the delivery schedule. Cutter heads, guide parts and remote commissioning support are available with every order.