Product Details
Place of Origin: Qingdao
Brand Name: Xinmeiteng
Certification: CE
Model Number: C518
Payment & Shipping Terms
Minimum Order Quantity: 1 Set
Price: Inquiry
Packaging Details: TO BE DETERMINED
Delivery Time: 45 working days after downpayment
Payment Terms: L/C,T/T
Supply Ability: 3 sets per season
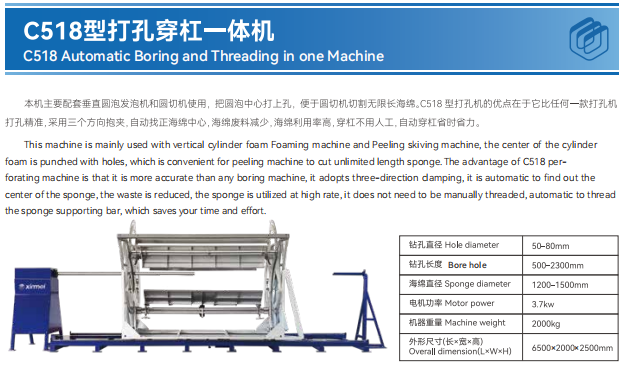
Motor Power: |
3.7 KW |
Hole Diameter: |
50-80 Mm |
Bore Hole Length: |
500-2300 Mm |
Sponge Diameter: |
1200-1500 Mm |
Machine Weight: |
2000 Kg |
Overall Dimension: |
6500*2000*2500 Mm |
Motor Power: |
3.7 KW |
Hole Diameter: |
50-80 Mm |
Bore Hole Length: |
500-2300 Mm |
Sponge Diameter: |
1200-1500 Mm |
Machine Weight: |
2000 Kg |
Overall Dimension: |
6500*2000*2500 Mm |
The C518 bores a shaft hole and threads it in one cycle. Bore hole length is 500-2300 mm, hole diameter is 50-80 mm, sponge diameter is 1200-1500 mm, motor power is 3.7 kW and machine weight is 2000 kg. The machine uses 3-direction clamping with automatic center positioning.
A bored roll that still needs a thread is a roll that has to be handled twice. Moving it to a second station costs a lift, a re-clamp and another chance to lose the centre line. The C518 bores and threads in the same clamping, so the thread follows the bore that was just cut.
One clamping, one centre line, two operations.
Full-length shaft holes threaded in the same pass.
The threading unit follows the bore without re-setting.
The roll stays fixed between boring and threading.
Check the thread at the entry, not only the bore depth. A thread that starts damaged will fail at assembly even if the bore is perfect.
Two operations on two machines mean the roll is lifted, moved and clamped twice. Each move is a handling cost, and each re-clamp is a chance to lose the centre line that was set at the first station.
Boring and threading in one clamping removes the second move. The thread is cut in the bore that was just made, so the thread axis and the bore axis are the same by construction rather than by alignment.
That shows up in the finished part. A threaded roll from a two-station process can have a thread that is slightly off the bore axis, which is enough to make a shaft bind at assembly. A single-cycle roll does not have that failure mode.
| Parameter | Value |
|---|---|
| Model | C518 |
| Machine type | 3-direction clamping foam drilling machine |
| Bore hole length | 500-2300 mm |
| Hole diameter | 50-80 mm |
| Sponge diameter | 1200-1500 mm |
| Clamping | 3-direction clamping |
| Positioning | Automatic center positioning |
| Motor power | 3.7 kW |
| Machine weight | 2000 kg |
| Overall dimension | 6500*2000*2500 mm |
| Certification | CE |
| Symptom | Likely cause | Action |
|---|---|---|
| Bore runs off centre | Roll not clamped square or centre height wrong | Re-clamp the roll and reset the centre height |
| Hole diameter out of tolerance | Worn or damaged cutter head | Fit a new cutter head and re-check |
| Thread damaged at the entry | Threading feed too fast | Reduce the threading feed rate |
| Roll slips during boring | Clamp pressure too low | Increase clamp pressure and check the pads |
| Spindle vibration | Worn bearing or loose drive belt | Check bearing play and belt tension |
| Torn bore surface | Dull cutter or feed too fast | Replace the cutter and reduce the feed |
Boring faults on a clamped drilling machine are usually set-up faults. Check clamping, centre height and cutter condition before adjusting the machine, because those three cause most rejects.
Keep hands clear of both the cutter and the threading unit. Two tools work in the same zone, and the threading unit moves after the bore is complete.
Stop the spindle before releasing the clamps. The roll must not move while either tool is in the bore.
The threading tool wears faster than the cutter and is the part that decides whether the thread passes inspection. Check it at the start of each batch and replace it on condition rather than on a fixed calendar.
The clamping and centring system needs the same attention as on the boring-only version. Check the pads monthly and confirm the centre position after any work on the clamps.
The machine ships in a reinforced export crate with the frame, clamping units and threading head braced for transport.
The shipment includes the tooling specification, layout drawing and a commissioning checklist, with remote support during installation.
A: Yes, boring and threading are done in one clamping cycle.
A: 500-2300 mm, with the thread cut in the same cycle.
A: 50-80 mm.
A: The thread follows the bore axis, so shafts do not bind at assembly.
Tell us the foam type, block or roll diameter, required hole diameter and the boring length you need. We will confirm the machine configuration, quote it and share the delivery schedule. Cutter heads, guide parts and remote commissioning support are available with every order.